Test Background and Objective
In micro-precision machining, when tool diameters shrink below 0.1mm, the contact force (trigger force) during the tool setting process becomes a critical variable affecting both tool life and machining accuracy. Many manufacturers, faced with the need to measure micro tools, turn to prohibitively expensive laser tool setters—often costing hundreds of thousands of dollars and placing a heavy burden on small and medium-sized factories.
This test aims to validate whether the TSENSE/BALLSUM tool setter, equipped with the appropriate low-force specification, can safely measure ultra-small tools with diameters of just 0.05mm—providing customers with a far more cost-effective tool setting solution.
Core Problem: Conventional contact tool setters typically have a trigger force of 2.5N–3.5N. For micro tools with diameters below 0.1mm, this force is sufficient to cause irreversible damage at the moment of contact. The T-SENSE 0.5N low-force tool setter was developed specifically to address this pain point.
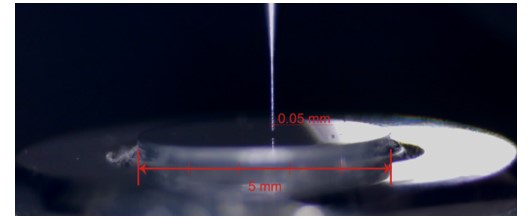
Test Environment and Parameters
| Tool Setter Brand | TSENSE / BALLSUM |
| Tool Brand | Taikee |
| Tool Specification | Ultra-micro grain carbide flat end mill, diameter 0.05mm |
| Feed Rate | 3mm/min (constant speed) |
| Test Personnel | T-SENSE Technical Team |
| Test Date | 2024.05.09 |
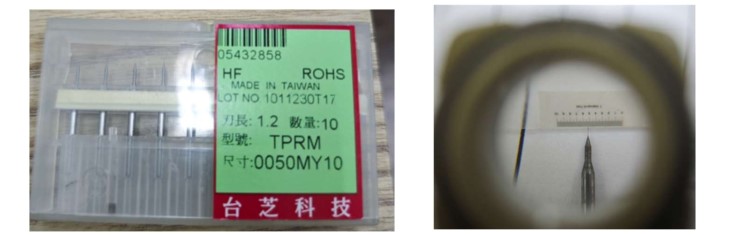
Detailed Tool Specifications
| Model | TPRM 0050MY10 |
| Cutting Diameter | 0.05mm (ultra-small diameter) |
| Effective Length | 0.10mm |
| Shank Diameter | 4mm |
| Flute Length | 1.2mm |
| Number of Flutes | 2 flutes |
| Length-to-Diameter Ratio | 24:1 |
| Material | Ultra-micro grain carbide substrate with wear-resistant coating designed for high-hardness mold steel (HRC 50+); high rigidity but elevated brittleness. |
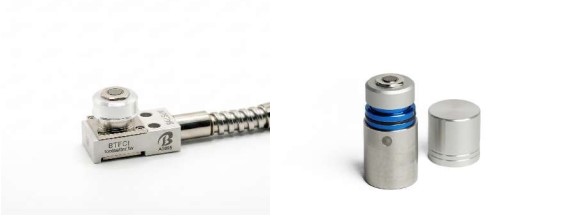
Detailed Tool Setter Specifications
| Model | BTFC1, BTS-5 |
| Contact Face Diameter | 5mm |
| Repeatability | 0.0006mm (2σ) |
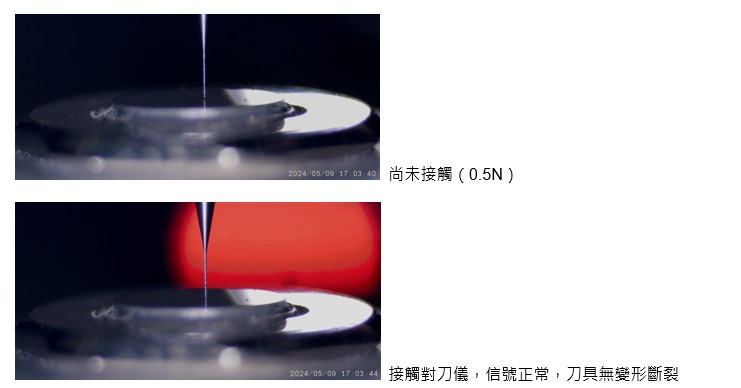
| Trigger Force | 0.5N (low-force specification) |
Test Results and Analysis
| Spring Force Level | Tool Condition | Test Result | Physical Explanation |
|---|---|---|---|
| 0.5N | No damage | Pass ✓ | Trigger signal sensitive. Tool tip examined under microscope shows no visible deformation at macro or micro scale. Tool retains full geometric integrity; safe to use for tool setting. |
| 0.82N | Slight plastic deformation | Caution ⚠ | Axial pressure on the tool has exceeded the material yield point, causing minor bending deformation. This deformation is barely visible to the naked eye but will directly affect subsequent machining dimensional accuracy. |
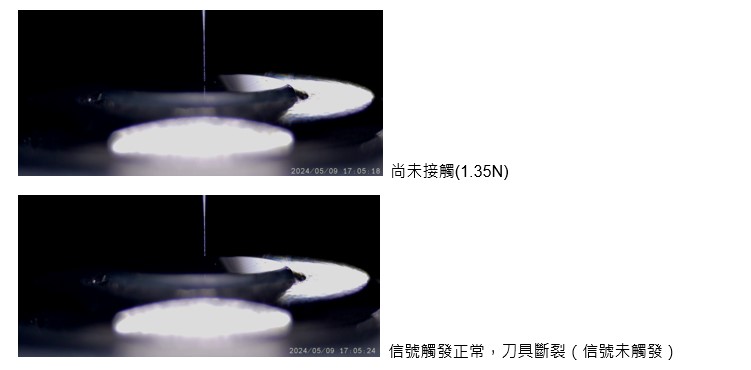
| 1.35N | Direct fracture | Fail ✗ | Contact stress at the moment of touch exceeds the ultimate strength of the ultra-micro grain carbide material, causing brittle fracture. The tool setting signal may still trigger, but the tool is destroyed and unusable. |
In-Depth Analysis
Tool Setter Preload Adjustment
Given the tool's length-to-diameter ratio of 24:1, the static trigger force of the tool setter must be calibrated to below 0.5N. Using a conventional tool setter with spring force above 2.5N would result in a near-100% tool breakage rate.
Feed Rate Optimization
This test used a constant feed rate of 3mm/min. In actual production environments, considering machine vibration and dynamic impact, a more conservative 1–2mm/min feed is recommended for initial tool setting to alleviate stress concentration along the extra-long cutting portion.
Run-Out Requirements
Ultra-high aspect ratio tools are extremely sensitive to spindle run-out. It is recommended to verify that spindle run-out is below 0.002mm before tool setting; otherwise, even with an appropriately low tool setter trigger force, lateral forces may still cause chipping at the tool tip at the moment of contact.
Conclusion
This test conclusively demonstrates that for the TPRM 0050MY10 ultra-small diameter end mill, the TSENSE/BALLSUM 0.5N low-force tool setter is essential to ensure measurement accuracy while protecting tool integrity. Any trigger force exceeding 0.5N will cause irreversible geometric damage to micro tools with such a high length-to-diameter ratio.
The 0.5N low-force specification of T-SENSE tool setters is a necessary condition for safe tool setting of 0.05mm diameter tools. No expensive laser tool setter is needed—equip your micro-precision machining line with a reliable tool measurement solution today.
Want to Learn More About Low-Force Tool Setters?
Contact us now for the most suitable tool setter specifications and pricing tailored to your machining requirements
Contact Us for Product Information